How to choose an automatic silk screen machine for production lines
Start with the job, not the machine brochure
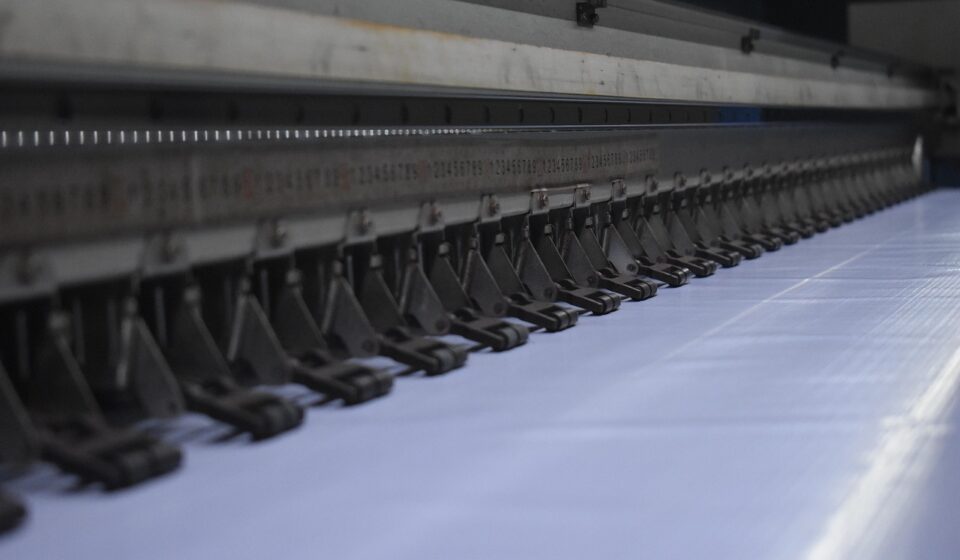
Choosing an automatic silk screen machine should start with the product and production conditions, not with the highest advertised speed or the largest color count. The right machine must hold the substrate accurately, cover the required image area, cure or dry the ink properly, change over within an acceptable time and run safely with the operators available in the plant. For many buyers, the real decision is not simply automatic versus manual. It is whether the machine format, fixtures, controls and after-sales support match the actual production mix.
This guide focuses on industrial buying decisions for bottles, panels, containers, electronic parts, glass, metal, plastics and other manufactured items. For more machinery purchasing topics, see our buying guides.
Define the product before defining the machine
Silk screen printing looks simple from the outside: ink passes through a prepared mesh screen onto a substrate. In production, the machine has to solve several mechanical problems at the same time. It must position the part, control the screen stroke, manage ink flow, keep registration stable and release the printed item without smearing. If any of these steps are unstable, automation only produces defects faster.
Substrate shape and holding method
The first specification should describe the part itself: dimensions, material, surface shape, weight, tolerance and how it can be held. Flat sheets, glass panels and nameplates usually suit flatbed screen printing. Cylindrical bottles, tubes and cups may require a round or curved-surface printing system with synchronized rotation. Irregular molded parts may need custom fixtures, nests, vacuum holding or servo-driven positioning.
Fixtures deserve more attention than they often receive. A machine can have excellent motion control, but if the product shifts during the print stroke, print quality will still drift. Ask the supplier to explain how the fixture locates the part, how quickly it can be loaded, whether it touches a cosmetic surface and how much tolerance variation it can accept.
True output instead of catalog speed
Catalog speed is usually measured under controlled conditions. Practical output depends on loading, unloading, ink behavior, screen cleaning, curing time, color changes, inspection and stoppages. A machine rated for high cycles per hour may still become a bottleneck if the operator cannot load parts consistently or if the ink needs a long flash-off time before handling.
A useful purchasing method is to calculate output from the full cycle: load, locate, print, unload, cure or dry, inspect and pack. If several colors are involved, include intermediate drying and registration checks. This avoids a common buying mistake: purchasing a fast printer while ignoring a slower process before or after it.
Compare machine formats before comparing prices
There is no universal automatic silk screen machine for every factory. The correct format depends on product geometry, order repeatability, color count and integration needs.
| Machine format | Best suited for | Main advantage | Key limitation to check |
|---|---|---|---|
| Automatic flatbed screen printer | Flat panels, labels, sheets, glass, metal plates and plastic parts | Stable print area and relatively simple tooling | Part flatness, vacuum holding and registration accuracy |
| Automatic cylindrical screen printer | Bottles, tubes, cups and round containers | Screen stroke can be synchronized with part rotation | Diameter range, taper, ovality and fixture changeover |
| Rotary indexing machine | Repeat products with higher volume | Multiple stations can combine loading, printing, drying and unloading | Less flexible for frequent product changes |
| Multi-color automatic line | Products requiring several registered colors | Improves repeatability across colors when properly set up | Higher tooling, setup and control complexity |
| Integrated line with handling equipment | Plants connecting printing to upstream or downstream processes | Reduces manual handling and work-in-process delays | Requires careful layout, safety review and maintenance planning |
The practical conclusion is straightforward: choose the simplest format that can meet the required quality, volume and changeover needs. Over-automation can add cost and downtime when orders are short and variable. Under-automation can limit growth when the same product is printed every day in repeat batches.
Build a specification from measurable requirements
A clear specification protects both buyer and supplier. Instead of asking for a “good machine,” define what the machine must do and how acceptance will be judged. This reduces misunderstandings during quotation, factory testing and installation.
Print area, color count and registration
Specify the maximum print area, minimum print area, artwork position tolerance and color-to-color registration requirement. If the product has logos, warning marks, scales or functional markings, registration tolerance may matter more than speed. For multi-color work, ask how each color is aligned and how the machine compensates for screen stretch, fixture variation or product tolerance.
Also define the screen frame size, mesh range and squeegee length. These details affect ink deposit, edge definition and long-term consumable cost. A supplier should be able to confirm whether standard screen frames are suitable or whether custom frames are required.
Ink, curing and material compatibility
Ink selection affects the entire production cell. Solvent-based, UV-curable and specialty inks may require different drying, ventilation, lamp systems, conveyor layouts or material handling methods. The printed substrate may also need pretreatment, such as flame, corona, plasma or cleaning, depending on material and surface energy.
Do not evaluate the printer separately from curing. A print that looks good at the machine exit can still fail adhesion, abrasion or chemical resistance requirements after handling. For critical products, buyers should define the test method used for acceptance, such as cross-hatch adhesion, rub resistance, solvent resistance or customer-specific inspection criteria.
Changeover and cleaning
Changeover time is a major cost driver in high-mix production. Ask how long it takes to replace fixtures, screens, squeegees and ink trays. Check whether adjustments are mechanical, pneumatic or servo-controlled, and whether recipes can be stored in the control system.
Cleaning should be part of the buying discussion as well. Ink pans, flood bars, squeegees and screens must be accessible without unsafe reaching or excessive downtime. If the machine is difficult to clean, operators may delay cleaning and quality may suffer.
Check automation quality, controls and safety
Automation quality is more than the number of cylinders or motors on the machine. It includes repeatable motion, stable fixtures, reliable sensors, clear alarms, maintainable wiring and safe access for operators. A well-designed automatic machine should make the process easier to control, not harder to understand. See also: factory planning.
Motion control and repeatability
Look at how the print stroke is driven and adjusted. Pneumatic systems can be cost-effective and simple, while servo systems may provide more precise control of speed, position and motion profiles. The right choice depends on the process. A simple single-color marking operation may not need advanced servo control, while multi-color or curved-surface printing may benefit from better synchronization.
Ask suppliers to demonstrate repeatability over a realistic run, not only on a single sample. Useful evidence includes sample sets from the beginning, middle and end of a test run, records of reject causes and video showing normal operating speed.
Guarding, interlocks and emergency stops
Safety should be reviewed early, especially when the machine includes moving tables, rotating fixtures, indexing stations, dryers or automatic loading. In the United States, OSHA 29 CFR 1910.212 is commonly referenced for general machine guarding requirements, including protection from hazards at the point of operation and other moving parts. ANSI B11.19 is often used as a reference for safeguarding and risk-reduction measures, while ISO 13849-1 is a recognized reference for safety-related control systems.
Those references do not replace a site-specific risk assessment, but they help buyers ask better questions. Does the machine have guards around pinch points? Are interlocked doors monitored correctly? Are emergency stops accessible from normal operator positions? Can maintenance staff safely clear jams and replace tooling? These questions should be answered before a purchase order is issued, not after installation.
Evaluate supplier evidence, not just model names
Two machines with similar names can perform very differently. The difference may come from frame rigidity, bearing quality, controls, fixture design, assembly quality, electrical documentation or service responsiveness. Buyers should request evidence that relates directly to their own parts.
- Sample printing test: Provide actual substrates, ink requirements and artwork instead of relying only on generic samples.
- Acceptance criteria: Define registration, coverage, edge quality, adhesion, reject rate and inspection method before testing.
- Cycle-time breakdown: Ask for measured times for loading, printing, unloading, curing and changeover.
- Technical documents: Request drawings, electrical diagrams, pneumatic diagrams, spare parts lists and operation manuals.
- Maintenance access: Confirm how screens, fixtures, squeegees, sensors and wear parts are adjusted or replaced.
- Training plan: Clarify what operators and maintenance technicians will learn during installation and commissioning.
For custom machinery, the factory acceptance test is especially important. It should use agreed materials and a realistic cycle, not a short demonstration with ideal samples. If the supplier cannot run the exact product, the quotation should clearly state what remains unverified.
Compare total cost of ownership and payback
The purchase price is only one part of the investment. A lower-priced automatic silk screen machine may become expensive if it needs frequent adjustment, custom consumables or long stoppages. A higher-priced machine may be justified if it reduces scrap, labor intensity, rework or floor-space constraints. The decision should be based on total cost of ownership.
| Cost item | Why it matters | Question to ask |
|---|---|---|
| Fixtures and tooling | Product-specific holding often determines print quality | Are fixtures included, and how much do extra sets cost? |
| Drying or curing | Ink performance depends on correct process conditions | Is a dryer, UV unit or conveyor required? |
| Utilities | Compressed air, power and ventilation can affect installation cost | What are the real operating requirements? |
| Consumables | Screens, squeegees, solvents and wear parts affect long-term cost | Are parts standard and easy to source? |
| Training and maintenance | Poor setup can reduce the value of automation | Who supports installation, troubleshooting and preventive maintenance? |
| Downtime risk | A stopped automatic line can block downstream production | Which critical spares should be kept on site? |
A simple payback review can compare current labor, scrap and throughput against expected improvements. Avoid using optimistic numbers that assume perfect uptime from day one. It is more realistic to include a learning period, preventive maintenance time and the cost of rejected parts during setup.
Use a decision matrix before issuing a purchase order
A decision matrix helps buyers avoid choosing only by price or brochure speed. Weight the factors that matter most to the production line and score each supplier against the same requirements.
| Evaluation factor | Suggested weight | What strong evidence looks like |
|---|---|---|
| Product fit and fixture design | 25% | Supplier demonstrates stable holding on real parts |
| Print quality and registration | 20% | Samples meet agreed tolerance and appearance criteria |
| Throughput and changeover | 15% | Measured cycle time includes loading, unloading and cleaning |
| Safety and maintainability | 15% | Guards, interlocks, access points and documentation are reviewed |
| Service and spare parts | 15% | Clear response plan, parts list and training support are provided |
| Total cost of ownership | 10% | Quotation includes tooling, utilities, consumables and optional equipment |
The weights can be adjusted. A cosmetics packaging plant may place more weight on appearance and registration. A parts manufacturer printing simple marks may prioritize uptime and quick fixture changes. What matters is that the decision reflects the production reality rather than a generic machine ranking.
Frequently asked questions
Is an automatic silk screen machine always better than a semi-automatic machine?
No. Automatic machines are usually stronger for repeatable volume, consistent cycles and lower manual printing labor. Semi-automatic machines may be better when batches are small, products change often or the budget cannot support fixtures, conveyors and additional automation.
What information should be sent to a supplier before quotation?
Send product drawings or dimensions, material, photos, artwork, print area, color count, required output, ink type if known, quality standards, available floor space and utility conditions. If possible, send real sample parts for print testing.
How much capacity headroom should a buyer plan for?
Plan enough headroom for normal growth and downtime, but do not buy excessive capacity without repeat orders to support it. A practical approach is to compare current demand, confirmed future programs and the cost of running a second shift or adding another machine later.
Which safety details are most important during evaluation?
Check guarding around moving parts, access to emergency stops, interlocked doors, safe maintenance access, clear lockout procedures and operator visibility. The final safety review should match local regulations and the conditions of the actual installation site.