Gear manufacturing explained from cutting and heat treatment to inspection
What gear manufacturing includes
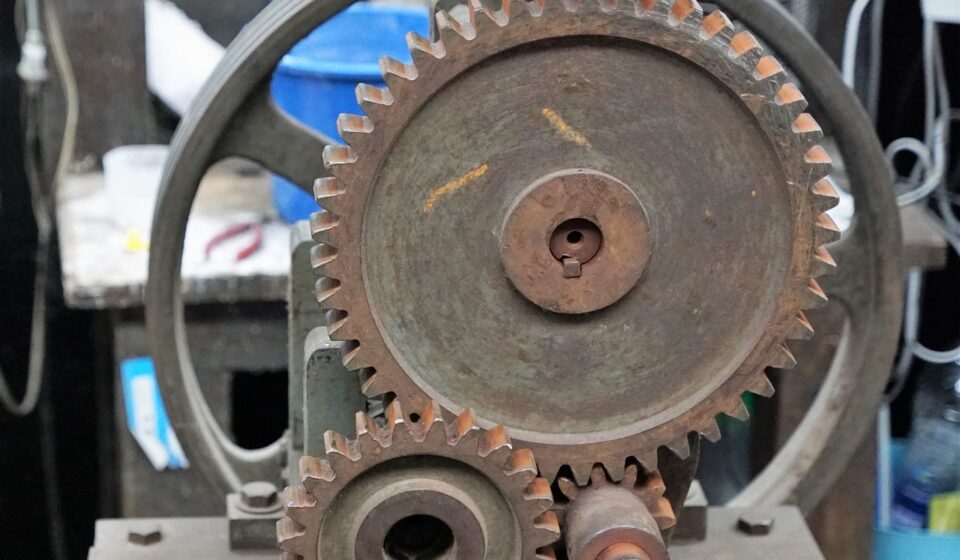
Gear manufacturing is the controlled route used to turn a gear design into a working mechanical component with the required tooth geometry, strength, surface finish and accuracy. A typical route starts with material and blank preparation, then moves through datum machining, tooth generation or forming, deburring, heat treatment, hard finishing and inspection. The key decision is not which process is universally best. It is which sequence can meet the load, noise, life, tolerance, volume and cost requirements of a specific gear. A conveyor reducer gear, a robot joint internal gear and a carburized transmission gear may all need different process routes. For related process explainers, see the manufacturing processes archive.
The typical gear manufacturing route
Most industrial gear production is a chain of dependent operations. Each step changes the risk profile of the part. A cutting process may generate an accurate involute profile, but later heat treatment can distort the teeth. A finishing operation may correct flank errors, but it cannot always rescue a blank with poor datum control. For that reason, gear manufacturing is best treated as a process system rather than a single machine operation.
| Stage | Purpose | Main risk to control |
|---|---|---|
| Gear data and tolerance definition | Define module or diametral pitch, tooth count, pressure angle, helix angle, face width, material and accuracy grade. | Ambiguous standards, missing inspection criteria or unrealistic tolerance targets. |
| Blank production | Create the basic disk, shaft, ring or near-net shape by bar stock machining, forging, casting, powder metallurgy or other methods. | Poor material quality, residual stress, excess stock or weak datum surfaces. |
| Datum machining | Machine bores, faces, journals and locating surfaces before tooth cutting. | Runout and misalignment that will carry into the tooth geometry. |
| Tooth generation or forming | Produce the gear teeth by hobbing, shaping, broaching, milling, skiving, grinding or related processes. | Profile error, pitch error, tool wear, burrs and process instability. |
| Deburring and chamfering | Remove burrs and protect tooth edges before handling, heat treatment and assembly. | Edge damage, inconsistent chamfers or loose burrs entering later operations. |
| Heat treatment | Improve wear resistance, fatigue strength or core strength through carburizing, nitriding, induction hardening, through hardening or carbonitriding. | Distortion, hardness variation, inadequate case depth or cracking. |
| Hard finishing | Improve final tooth accuracy and surface condition by grinding, honing, lapping or shaving where applicable. | Grinding burn, overcorrection, surface damage or loss of flank modification. |
| Inspection | Verify profile, helix, pitch, runout, tooth thickness, surface condition, hardness and other specified requirements. | Using an accuracy label without checking the actual parameters needed for the application. |
Main tooth-forming and tooth-cutting methods
Hobbing
Hobbing is one of the most common methods for external spur and helical gears. A hob rotates in a generating relationship with the gear blank and progressively creates the tooth spaces. The process is productive for many cylindrical gears because it is continuous and can be automated. It is not suitable for every geometry, however. Internal gears, gears with obstructed shoulders and some special profiles may require shaping, skiving, broaching or milling instead.
Shaping, broaching and power skiving
Gear shaping uses a gear-like cutter in a reciprocating motion. It is often selected for internal gears, shoulder gears and features that do not provide the cutter clearance needed for hobbing. Broaching is fast for high-volume internal splines or simple internal forms, but the tool investment is high and flexibility is limited. Power skiving has gained attention because it can cut internal and external cylindrical gears with high productivity when the machine, workholding, tool design and synchronization are rigid enough. It is not a casual substitute for every shaping job. The process depends heavily on machine stiffness, tool geometry, collision control and simulation.
Milling, grinding and special processes
Form milling and 5-axis CNC machining are useful for prototypes, repair parts, large gears, low-volume work and unusual geometry. They may not match the productivity of dedicated generating processes in large batches, but they offer flexibility. Gear grinding can also generate teeth, although it is more often used as a finishing operation after heat treatment when high accuracy, lower noise or improved surface condition is required. Wire EDM, additive manufacturing and powder metallurgy can play roles in special cases, but high-load metallic gears usually still require careful finishing, material validation and inspection before use in demanding power transmission.
Materials and heat treatment decisions
Material selection affects every later operation. Low-carbon alloy steels are often selected for carburized gears because they can develop a hard wear-resistant case while retaining a tougher core. Medium-carbon alloy steels may be through hardened or induction hardened when full-section strength or localized tooth hardening is more appropriate. Stainless steels, cast irons, bronzes, engineering plastics and powder metal materials can also be used, depending on corrosion, lubrication, noise, weight, cost and duty cycle requirements.
Heat treatment is often the dividing line between a simple machined component and a durable power-transmission gear. ASM International references on gear heat treatment describe commonly used methods such as through hardening, carburizing, nitriding, carbonitriding and induction hardening. Carburizing is widely used where high surface durability and bending fatigue performance are required. Nitriding is valued where dimensional stability is important because it can create a hard surface with less distortion than quench-based processes. Induction hardening is useful when the hardening pattern must be concentrated around the tooth surface or root area.
The practical limitation is distortion. Heating, quenching and phase transformation can change tooth geometry, bore alignment and runout. For precision gears, manufacturers often leave grinding stock before heat treatment and then finish the flanks after hardening. The stock allowance must be enough to clean up distortion, but not so large that finishing becomes slow, expensive or thermally risky.
Accuracy standards and inspection
Gear quality should be specified by standard, edition and measurable parameters, not by a vague phrase such as precision gear. ISO 1328-1:2013 defines a flank tolerance classification system for individual cylindrical involute gears and uses classes numbered 1 to 11 in order of increasing tolerance. In simple terms, lower class numbers represent tighter flank tolerances. The standard addresses manufacturing and conformity assessment of tooth flanks; it does not, by itself, guarantee gearbox performance, noise level or service life.
AGMA accuracy designations require similar care. Older ANSI/AGMA 2000-A88 quality numbers used Q designations in which a higher number indicated greater precision. Later AGMA systems aligned more closely with ISO-style numbering, where increasing numbers mean decreasing precision. This creates a real communication risk. A gear drawing, purchase order or inspection report should identify the exact standard and edition, not just a grade number.
Inspection may include profile deviation, helix deviation, single pitch deviation, cumulative pitch deviation, runout, tooth thickness, lead crown, surface texture, hardness, case depth and metallurgical checks. Functional testing, such as single-flank or double-flank rolling, can be useful, but it should not replace elemental inspection when the drawing calls for specific flank tolerances. For safety-critical or high-load gearing, documentation may also include material certificates, heat treatment records, magnetic particle inspection, grinding burn checks and traceability records.
How to choose a gear manufacturing process
The best process route depends on five practical questions. What geometry is required? How many gears will be produced? What accuracy and noise level are expected? Will the gear be hardened? What inspection evidence is required? The answers usually narrow the route faster than a general comparison of machine types. See also: buying guides.
| Application need | Likely process route | Why it fits |
|---|---|---|
| Prototype or replacement gear | CNC milling, wire EDM, form cutting or limited hobbing | Flexibility matters more than maximum cycle-time efficiency. |
| External spur or helical gear in batch production | Blank machining, hobbing, deburring and finishing as needed | Hobbing is productive and well established for many external cylindrical gears. |
| Internal gear or spline | Shaping, broaching or power skiving | Tool access and internal geometry limit the use of hobbing. |
| High-strength hardened gear | Cut teeth before heat treatment, carburize or harden, then grind or hone | Hard finishing compensates for heat treatment distortion and improves flank condition. |
| Large open gearing | Forged or cast blank, rough machining, hobbing or milling, localized hardening and inspection | Size, handling, tooth access and heat treatment capacity drive the route. |
| Low-noise precision drive | Controlled cutting, flank modification, hard finishing and detailed inspection | Profile, lead, pitch, surface finish and assembly effects all influence noise and vibration. |
Trends shaping gear manufacturing
Three trends are especially important. First, power skiving and multifunction machines are expanding process options for internal gears, splines and compact drive components. This matters for robotics, electric mobility and precision automation, where compact gearboxes often contain internal gear features and strict noise requirements. The benefit is not only cycle time; it is the ability to combine turning, gear cutting, chamfering and measurement more tightly in one production concept.
Second, closed-loop manufacturing is becoming more valuable. Modern gear measuring systems can feed correction data back to cutting or grinding machines. That does not remove the need for process knowledge, but it reduces trial-and-error adjustment and helps stabilize production. For gears affected by heat treatment distortion, the ability to compare pre-heat and post-heat data is a practical advantage.
Third, additive manufacturing is useful, but it should be treated realistically. ISO and ASTM additive manufacturing terminology and qualification standards provide a framework for discussing 3D printing processes, materials and production qualification. Additive methods can help with prototypes, lightweight forms, tooling aids and special low-volume components. For high-load gears, however, the printed part still has to meet the same demands for density, surface integrity, heat treatment response, flank accuracy and fatigue performance. In many cases, printing is a blank-making or development tool rather than a direct replacement for precision gear cutting and finishing.
Common mistakes to avoid
- Specifying a grade without a standard. Always identify the accuracy standard and edition, especially when AGMA and ISO terminology may be mixed.
- Ignoring datum quality. Tooth accuracy depends on the bore, faces and locating surfaces used during cutting and inspection.
- Leaving heat treatment out of the process plan. Hardening can change size and geometry, so stock allowance and final finishing must be planned early.
- Assuming grinding fixes every problem. Grinding can improve flank geometry and surface condition, but it cannot correct poor material selection, weak root design or excessive distortion without consequences.
- Choosing a process only by unit price. Tooling cost, inspection effort, scrap risk, setup time and repeatability often matter as much as machine cycle time.
Frequently asked questions
What is the most common gear manufacturing process?
For many external spur and helical gears, hobbing is one of the most common and productive methods. It is not universal. Internal gears, shoulder gears, hardened precision gears and prototypes may require shaping, skiving, broaching, milling, grinding or other routes.
Is gear grinding always required?
No. Gear grinding is typically used when the gear must meet tight accuracy, surface finish, noise or post-heat-treatment requirements. Many lower-speed or less demanding gears can function with cut, shaved or otherwise finished teeth if the drawing and application allow it.
What is the difference between hobbing and shaping?
Hobbing uses a rotating hob in a continuous generating process and is efficient for many external cylindrical gears. Shaping uses a reciprocating cutter and is often chosen for internal gears or gears with limited cutter clearance near shoulders.
How does heat treatment affect gear manufacturing?
Heat treatment improves wear resistance, fatigue strength or hardness, but it can also distort the gear. Precision gears are often cut soft, heat treated, and then finished by grinding, honing or lapping to restore the required tooth accuracy.
Which standards define gear accuracy?
ISO 1328 is widely used for cylindrical gear flank tolerance classification, and AGMA standards are also common in industry. The key is to specify the exact standard, edition and inspection parameters so that buyer and manufacturer interpret the grade in the same way.