Precision cast components for machinery design and procurement
What precision cast components mean in machinery design
Precision cast components are metal parts made by a casting process where geometry, surface condition, dimensional tolerance, machining allowance, and inspection requirements are controlled closely enough for functional use in machinery. The term is often linked with investment casting, also called lost-wax casting, but the procurement issue is wider than the process name. The practical question is whether the part can be produced close to its final shape with less machining, less welding, and fewer assembled pieces than a fully machined or fabricated alternative. For readers comparing manufacturing routes across precision components, the value is not in the word precision itself. It comes from turning a functional design into measurable requirements that a foundry, machinist, and quality team can verify.
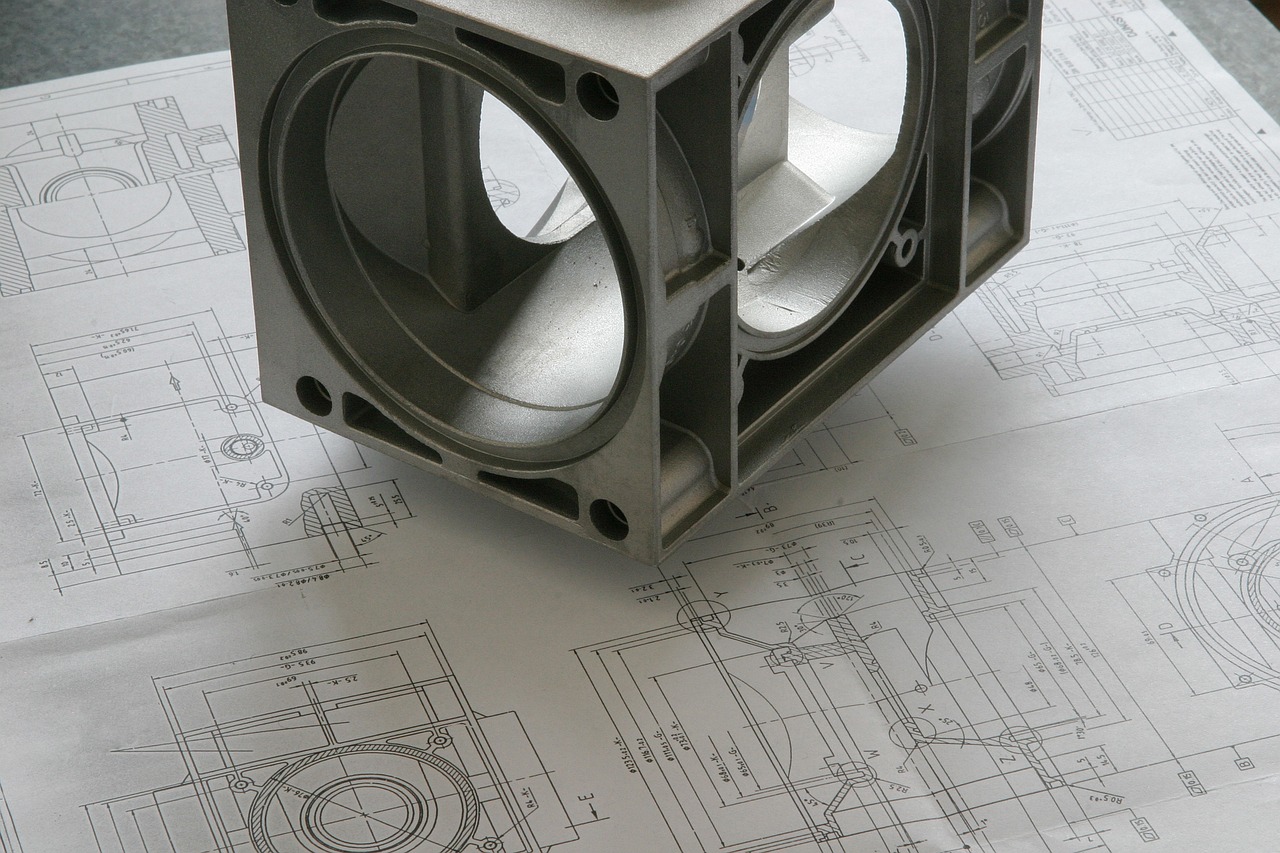
In engineering practice, a precision casting is not automatically a finished component. Some surfaces may be suitable as cast, while bearing seats, sealing faces, threaded holes, locating datums, or hydraulic interfaces may still require machining. The strongest designs treat casting and machining as one manufacturing route, not as separate decisions made after the drawing is complete.
Why casting precision is not only a foundry claim
Precision in casting is created through a chain of decisions. If one link is unclear, the final part may look correct but still fail fit, function, or repeatability requirements. Public technical material from the Investment Casting Institute describes investment casting as a process built around wax patterns, ceramic shell building, dewaxing, pouring, shell removal, and finishing. Each stage can affect the accuracy and repeatability of the final component.
Pattern and tooling decisions
The pattern defines the cavity that will later receive molten metal. Shrinkage allowance, wax injection consistency, gate design, core placement, and tooling wear all affect the final casting. For small and complex parts, multiple wax patterns may be assembled on a sprue to improve production economics. That assembly can improve throughput, but it also makes feeding, thermal balance, and part orientation important engineering choices.
Shell, mold, and metal behavior
Investment casting uses a ceramic shell built in layers around the pattern. The shell must be strong enough to withstand handling, dewaxing, burnout, and pouring, while still capturing fine geometry. In other casting routes, sand systems, permanent molds, or dies play similar roles. Metal behavior adds another level of complexity. Alloy chemistry, section thickness, pouring temperature, solidification rate, and heat treatment can affect dimensional movement, internal soundness, surface condition, and mechanical properties.
Machining allowances and inspection strategy
A near-net-shape casting may reduce stock removal, but it still needs enough material on critical surfaces for machining cleanup. Too much machining allowance wastes material and cycle time. Too little allowance creates scrap risk. Inspection strategy also matters because a raw casting cannot be evaluated in the same way as a fully machined part. Datums, rest points, stock distribution, and the sequence from casting inspection to machining verification should be discussed before tooling is finalized.
Standards and drawings that keep expectations measurable
Standards do not replace engineering judgment, but they help prevent vague purchasing language. ISO 8062-3:2023, published in February 2023, specifies general dimensional and geometrical tolerances and machining allowance grades for castings using plus-minus tolerances on indicated dimensions. Its scope covers castings in cast metals and alloys made by various casting processes, but it does not apply to 3D CAD models used without indicated dimensions. This distinction matters because a model alone may show nominal geometry without communicating the tolerance system needed for supplier evaluation.
For steel castings, Steel Founders Society of America guidance is often used as a practical reference when discussing dimensional tolerance and required machining allowance. The guidance emphasizes that many as-cast dimensions are matters for agreement between purchaser and producer. In other words, a drawing should not simply say precision casting and assume the supplier understands every functional requirement.
ASTM E29-22 is another useful reference in quality communication because it addresses the use of significant digits in test data when determining conformance with specifications. That may seem distant from casting design, but it matters whenever chemical analysis, mechanical testing, hardness, or inspection data are compared with acceptance limits. Rounding rules can change whether a reported value is judged conforming or nonconforming.
| Requirement area | What should be defined | Why it matters |
|---|---|---|
| Material | Alloy grade, specification, heat treatment, and any corrosion or temperature requirement | Controls strength, wear behavior, weldability, and service limits |
| Geometry | Critical dimensions, datums, draft expectations, core features, and wall thickness targets | Prevents over-reliance on a nominal 3D model |
| Tolerances | Applicable tolerance grade, individual critical tolerances, and geometric tolerances | Separates functional features from noncritical surfaces |
| Machining | Machined surfaces, stock allowance, datum sequence, and final surface finish | Reduces the risk of insufficient cleanup or unnecessary material removal |
| Inspection | Dimensional checks, sampling plan, material tests, and any nondestructive examination | Makes acceptance criteria clear before production |
When precision casting is a better fit than machining, fabrication, or additive manufacturing
Precision casting is usually worth evaluating when the part has complex external geometry, internal passages, curved surfaces, bosses, ribs, mounting features, or alloy requirements that would make machining from billet inefficient. It can also reduce assembly risk when a welded or bolted fabrication can be redesigned as a single casting. The benefit is strongest when the design works with the casting process rather than against it.
Machining remains a better choice for simple prismatic shapes, very tight datum relationships, extremely low quantities, or surfaces that require precision on nearly every face. Fabrication can be more economical for large structures made from plate, tube, or standard sections, especially when geometry is not too complex. Additive manufacturing can help with prototypes, tooling aids, cores, or complex metal parts, but public research from the National Institute of Standards and Technology continues to emphasize measurement science, model validation, and process-property relationships. That makes additive manufacturing a powerful option, not an automatic replacement for established casting routes.
| Design situation | Why precision casting may help | Limit to check early |
|---|---|---|
| Complex housing or bracket | Combines ribs, bosses, curves, and mounting features in one form | Datum plan and machining cleanup must be realistic |
| Fluid or pump component | Can form smoother curved passages than some fabricated assemblies | Internal inspection and core removal must be feasible |
| Wear or heat resistant alloy part | Can form alloys that are difficult or costly to machine from solid stock | Heat treatment and mechanical property verification are essential |
| Multi-piece welded assembly | May reduce welding distortion, fixture work, and leak paths | Tooling cost and design validation must justify the change |
| Prototype or short run | May work if tooling can be simplified or patterns can be produced efficiently | Lead time and unit cost may still favor machining or additive routes |
A procurement checklist before ordering precision cast components
Many quality problems begin before the first casting is poured. A purchasing package should tell the supplier what the part must do, which features are critical, and how conformance will be judged. The following checklist is a practical starting point for engineers, sourcing teams, and manufacturing planners.
- Provide a controlled drawing revision and, if used, a matching 3D model with clear authority between the two.
- Identify critical-to-function dimensions instead of applying unnecessarily tight tolerances across every surface.
- Specify the material grade, applicable material standard, heat treatment condition, and any hardness or mechanical test requirement.
- Define casting tolerance expectations, machining allowance, and surfaces that must remain as cast.
- Mark machined datums, final machined dimensions, surface finish requirements, and thread specifications.
- State whether first article inspection, dimensional reports, chemical analysis, mechanical testing, pressure testing, or nondestructive examination is required.
- Clarify acceptable cosmetic conditions separately from functional defects, because visual appearance and performance risk are not always the same.
- Discuss packaging, corrosion protection, traceability, and lot control if the component will enter regulated or safety-critical equipment.
This level of detail may take longer at the quotation stage, but it usually shortens the total project cycle. Suppliers can identify undercuts, thin sections, inaccessible cores, sharp internal corners, unrealistic tolerances, or machining risks before cost and lead time are locked in. See also: buying guides.
Common risks and how early design choices reduce them
Precision casting is a mature manufacturing route, but it is not risk-free. Industry defect references, including those published for investment casting, commonly classify problems such as non-metallic inclusions, finning, misruns, shrinkage, surface defects, and core-related issues. Naming these defects is not a warning against casting. It is a reminder that early process planning is part of achieving precision.
Porosity and shrinkage risk increase when heavy sections feed thin sections poorly or when isolated hot spots solidify late. Designers can reduce this risk by keeping wall thickness more uniform, adding radii instead of sharp corners, and allowing the foundry room for gates, risers, or process-specific feeding methods. Inclusions and shell-related defects can be influenced by shell integrity, handling, burnout, and pouring practice. Distortion can result from uneven cooling, heat treatment, or aggressive machining stock removal.
Another common risk is over-tolerancing. A drawing that demands machined-level tolerances on every as-cast feature may add cost in tooling, inspection, rework, and scrap without improving function. A better approach is to divide the part into functional zones: critical machined interfaces, controlled as-cast features, cosmetic surfaces, and noncritical stock areas. This lets the process deliver value where it matters most.
Frequently asked questions
Are precision cast components the same as investment castings?
Not always. Investment casting is one of the most common processes associated with precision cast components because it can produce complex near-net shapes with fine detail. However, the phrase precision cast components can also be used more broadly when a casting is engineered for controlled tolerances, surface condition, material properties, and downstream machining.
Do precision cast components still need machining?
Often, yes. Casting can reduce machining, but it rarely eliminates every secondary operation. Bearing seats, sealing faces, threaded holes, precision bores, and datum surfaces commonly need machining after casting. The key is to define which features must be machined and which can remain as cast.
How tight can casting tolerances be?
There is no single answer that applies to every alloy, part size, process, and geometry. Tolerance capability depends on the casting process, tooling, section thickness, part orientation, heat treatment, and inspection method. Drawings should reference an agreed tolerance system such as ISO 8062-3:2023 where appropriate, then add individual tolerances for features that truly control function.
What should be sent when requesting a quotation?
A strong request should include the drawing, 3D model if available, target material, annual or batch quantity, critical dimensions, machining expectations, surface finish needs, inspection requirements, and service conditions. If an existing machined or fabricated part is being converted to a casting, include the functional reason for the conversion so the supplier can suggest design changes.
Is additive manufacturing replacing precision casting?
Additive manufacturing is changing how some prototypes, tooling, cores, and metal parts are produced, but it has not made casting obsolete. In many machinery applications, the practical decision is not casting versus additive manufacturing in isolation. It is which route gives the right material, repeatability, inspection confidence, cost, and lead time for the required production volume.
Final takeaways for engineers and buyers
Precision cast components create value when the design uses casting to simplify geometry, reduce material waste, lower machining time, or consolidate assemblies. They create problems when precision is treated as a marketing label instead of a measurable agreement. The drawing, tolerance system, machining allowance, inspection plan, and supplier feedback loop determine whether a casting becomes a reliable machinery component.
The best early question is not simply whether a part can be cast. It is which surfaces must be precise, which features can remain as cast, what standards define acceptance, and how much process variation the design can tolerate. Answering those questions before tooling and sourcing decisions are finalized gives precision casting its strongest chance to reduce cost without reducing performance.