How to evaluate lathe machine tools for modern manufacturing
Why lathe machine tools still matter
Lathe machine tools shape material by rotating the workpiece against a cutting tool. They remain essential for shafts, bushings, fittings, threads, rollers, pins, and many other rotational parts. The process is long established, but the purchase decision is still complex: should a shop use a manual lathe, a CNC turning center, a Swiss-type machine, a vertical turning lathe, or a mill-turn platform?
The right answer is not automatically the newest or most automated option. It depends on the part mix, tolerance requirements, material behavior, setup frequency, operator skill, workholding, guarding, chip control, and the cost of downtime. This guide explains the main types of turning equipment, the practical points to compare before investment, and how safety and digital manufacturing trends affect machine selection on the shop floor.
For more manufacturing equipment topics, visit the machine tools section.
What counts as a lathe machine tool
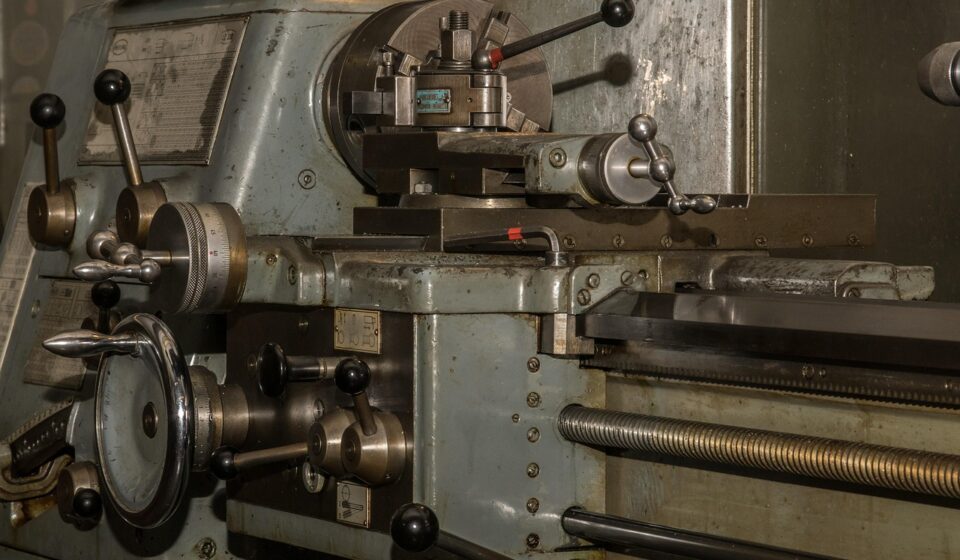
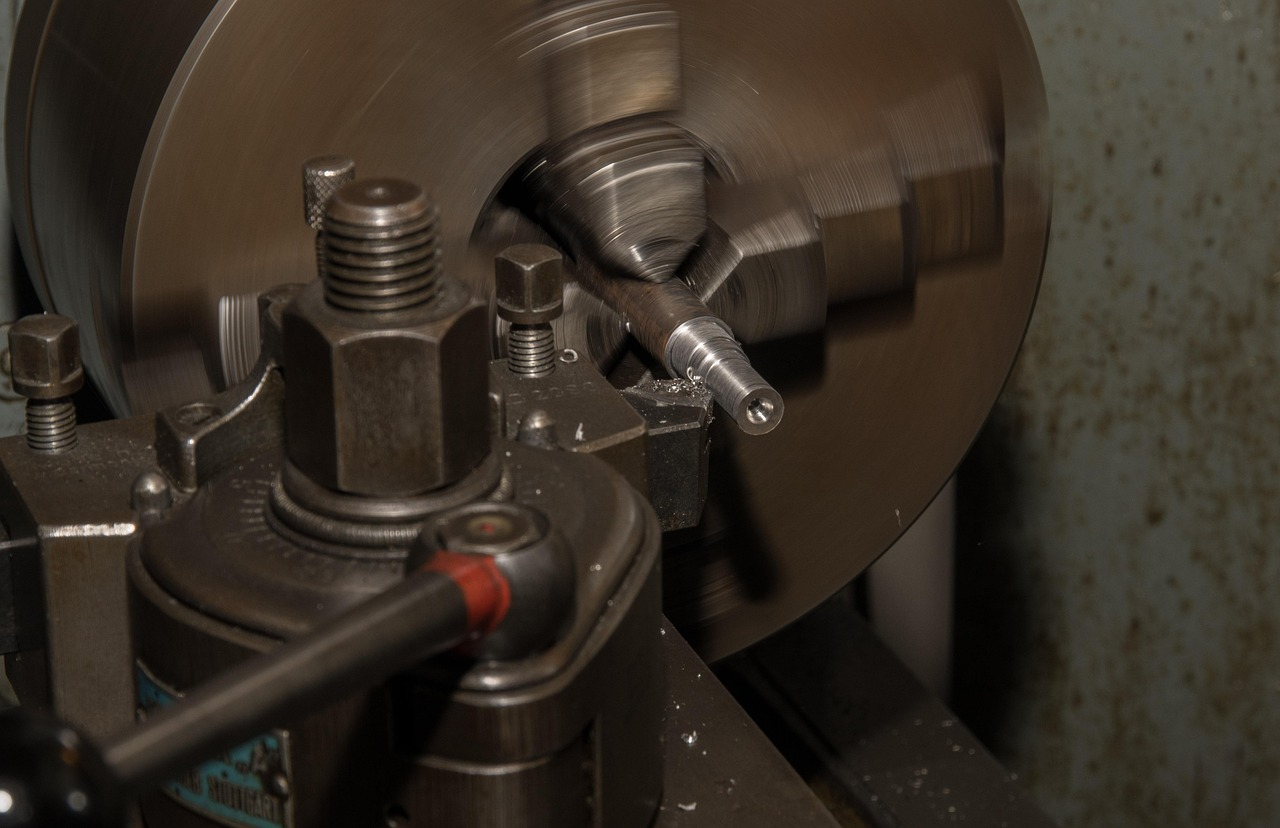
A lathe is a turning machine. In most metalworking applications, the workpiece is held in a chuck, collet, faceplate, fixture, or between centers. It rotates while a tool removes material. The cutting tool may be moved manually by an operator, guided by mechanical mechanisms, or controlled by CNC axes. The finished feature is usually round, conical, threaded, grooved, bored, or faced.
That simple definition covers a wide range of equipment. A training room may use a compact manual lathe to teach feeds, speeds, and tool geometry. A repair shop may rely on an engine lathe for one-off shafts and sleeves. A high-volume supplier may run CNC turning centers with bar feeders and part catchers. A shop making small, slender medical or electronic components may choose Swiss-type turning. A heavy manufacturing facility may need a vertical turning lathe for large rings, wheels, or flanges.
In practice, the word “lathe” should not be treated as a single machine category. It is more useful to evaluate lathe machine tools by capability: swing diameter, distance between centers, spindle bore, spindle speed range, torque, axis configuration, turret capacity, live tooling, sub-spindle capability, control system, coolant delivery, guarding, automation readiness, and service support.
Main types of lathe machine tools
The following comparison gives a practical view of common lathe categories. It is not a ranking, because each type is designed around a different production problem.
| Lathe type | Typical use | Main advantage | Common limitation |
|---|---|---|---|
| Engine or manual lathe | Repair work, prototypes, training, low-volume parts | Flexible and relatively simple to set up | Output depends heavily on operator skill and manual consistency |
| Toolroom lathe | Precision one-off parts, gauges, fixtures, maintenance parts | Better accuracy and finish than many general-purpose manual lathes | Not ideal for high-volume unattended production |
| Turret lathe | Repeating operations on similar parts | Faster tool changes than a basic manual lathe | Less flexible than modern CNC systems |
| CNC turning center | Batch production, repeatable turning, threading, boring, grooving | Repeatability, programmable control, automation options | Higher setup discipline, programming knowledge, and maintenance needs |
| Swiss-type lathe | Small-diameter, long, slender, high-precision components | Strong support near the cutting zone reduces deflection | Best suited to specific part families rather than all turning work |
| Vertical turning lathe | Large, heavy, short workpieces | Gravity supports heavy parts on a vertical table | Less appropriate for long shaft-type parts |
| Mill-turn machine | Parts requiring both turning and milling features | Can reduce secondary operations and handling | More complex programming, tooling, and collision control |
For many shops, the important distinction is not simply manual versus CNC. It is simple turning versus complete-part machining. A basic CNC lathe may be enough for round parts with limited cross-holes or flats. A turning center with live tooling may reduce transfers to a machining center. A mill-turn machine may improve accuracy between turned and milled features because more work is completed in one clamping. That benefit only matters, however, when the part mix justifies the extra cost and process complexity.
How to match the machine to the part
Strong machine selection starts with a part-family review, not a machine catalog. A shop should group parts by diameter, length, material, tolerance, feature complexity, annual volume, and setup frequency. This helps identify whether the real bottleneck is cutting time, setup time, inspection time, tool changes, workholding, or material handling.
Part geometry and work envelope
Swing diameter and distance between centers are basic specifications, but they are not enough. Spindle bore, chuck size, turret clearance, tailstock capacity, steady rest options, and bar feeder compatibility often decide whether a lathe can run a part safely and efficiently. Long shafts may need center support or steady rests. Thin-walled parts may require controlled clamping pressure. Heavy asymmetric parts may require lower speed, careful balancing, and stronger guarding.
Material and cutting conditions
Aluminum, brass, carbon steel, stainless steel, cast iron, titanium, and hardened materials behave differently during turning. Material affects spindle power, torque, insert grade, chip formation, coolant strategy, and surface finish. A machine with high maximum rpm may be attractive for small aluminum parts. For large steel components, higher low-speed torque may matter more. The better question is not “How fast is the spindle?” but “Does the spindle deliver useful power and rigidity at the speeds this part family needs?”
Tolerance, finish, and thermal stability
Repeatable precision depends on more than the control system. Bed design, spindle bearings, guideway construction, thermal behavior, servo performance, toolholding, workholding, and measurement routines all contribute to the result. Shops working to tight tolerances should consider warm-up routines, in-process measurement, tool wear offsets, coolant temperature control, and how often operators must intervene to maintain capability.
Safety and standards should shape the specification
Lathe safety is not an accessory issue. Turning operations involve rotating parts, clamping devices, cutting zones, chips, coolant, and sometimes long bar stock. OSHA’s general machine-guarding requirements in 29 CFR 1910.212 identify hazards such as the point of operation, rotating parts, ingoing nip points, flying chips, and sparks. ISO 23125:2015 is the international safety standard specifically addressing turning machines and turning centers. These references are useful because they frame the discussion around risk reduction, not operator convenience.
Important safeguards and operating controls may include interlocked doors, chuck guards, chip shields, emergency stop devices, spindle braking, bar stock containment, safe access for setup, and procedures that prevent measuring or clearing chips while the spindle is running. Vertical turning machines and CNC turning centers often use fixed or interlocked guarding during automatic cycles. Manual and semi-manual operations require closer attention to exposed rotating components and operator position.
Safety decisions should also account for the workpiece and workholding. Irregular jaws, protruding stock, long unsupported bar, or unbalanced parts can create hazards even when the machine itself is in good condition. A guard that works for short chucking operations may not be sufficient for long-bar work. A coolant splash shield does not necessarily control ejected parts. Shops should avoid treating any single shield, door, or warning sign as a complete safety system.
- Confirm that guarding covers the actual operation, not only the original machine configuration.
- Review chuck, jaw, collet, and fixture condition before production.
- Control access to rotating bar stock and unsupported projections.
- Use chip hooks, brushes, or approved tools instead of hands for chip removal.
- Train operators on setup, emergency stops, safe measurement, and restart procedures.
- Document changes when tooling, fixtures, automation, or part geometry changes the risk profile.
Automation and digital features are useful when they solve a real bottleneck
Modern lathe machine tools increasingly include features associated with smart manufacturing: CNC connectivity, tool life monitoring, spindle load monitoring, probing, bar feeding, robotic loading, automatic doors, part catchers, and production data collection. NIST describes smart manufacturing in terms of integrated information systems, real-time monitoring, interoperability, control, optimization, and rapid reconfiguration. In turning operations, those ideas create value only when they address a measurable shop problem. See also: buying guides.
A bar feeder can extend unattended run time for high-volume shaft or fitting production. A sub-spindle can reduce manual handling when both ends of a part need machining. Live tooling can eliminate a secondary milling setup. Probing can reduce scrap during setup or help compensate for tool wear. Monitoring spindle load can help detect tool breakage or abnormal cutting. Connectivity can help supervisors understand utilization, downtime causes, and maintenance needs.
Automation can also expose weak process control. If incoming material varies, workholding is unstable, chips jam around the tool, or programs are not proven, an automated cell may simply produce scrap faster. Before adding robots, pallet systems, or unattended shifts, shops should stabilize cutting data, fixture repeatability, tool life, chip evacuation, inspection plans, and recovery procedures.
Total cost matters more than purchase price
The initial purchase price is only one part of the economic picture. A lower-cost lathe may become expensive if it has poor support, limited tooling compatibility, weak chip control, high scrap rates, or long setup times. A more capable machine may be justified if it reduces secondary operations, improves first-pass yield, or allows one operator to manage more output. The practical comparison is total cost per acceptable part over the expected production life.
Key cost factors include machine price, installation, foundation or electrical work, tooling, workholding, coolant and filtration, inspection equipment, programming time, operator training, maintenance, replacement parts, energy use, floor space, scrap, downtime, and financing. For CNC machines, shops should also include post processors, simulation needs, network integration, and data backup procedures.
A useful evaluation method is to build three scenarios: current process cost, conservative improvement, and expected improvement. The conservative scenario matters because cycle-time savings alone can be misleading. If a new turning center reduces cutting time but setup, inspection, or deburring remain unchanged, the real improvement may be smaller than expected.
- For prototype work: prioritize flexibility, visibility, setup speed, and skilled manual control.
- For repeat batches: prioritize repeatability, tool management, quick changeover, and proven programs.
- For high-volume bar work: prioritize bar feeding, chip evacuation, tool life, part catching, and unattended reliability.
- For complex parts: prioritize live tooling, sub-spindle capability, collision avoidance, and programming support.
- For heavy parts: prioritize rigidity, low-speed torque, safe loading, workholding strength, and guarded access.
A practical checklist before selecting a lathe
Before choosing or upgrading turning equipment, decision-makers should move from general specifications to production evidence. The following checklist connects machine capability with actual manufacturing requirements.
- Define the top part families by diameter, length, material, tolerance, and annual volume.
- Identify whether the bottleneck is setup, cutting, inspection, tool life, chip control, or handling.
- Confirm the required work envelope with real fixtures, jaws, tools, and clearances included.
- Check spindle bore, torque curve, rpm range, and chuck capacity against actual parts.
- Review turning, boring, threading, grooving, drilling, milling, and part-off requirements.
- Decide whether live tooling, Y-axis, sub-spindle, tailstock, steady rest, or bar feeder capability is needed.
- Evaluate guarding, interlocks, emergency stops, chip containment, and access for setup.
- Estimate tooling, workholding, programming, training, maintenance, and inspection costs.
- Request sample cuts or cycle studies when the investment depends on a narrow performance claim.
- Plan operator training and maintenance routines before the machine reaches the floor.
The most successful lathe projects usually start with a clear process map, not a feature wish list. When a shop understands why parts fail, why setups take time, and why machines sit idle, it can select equipment that removes specific constraints. That approach is more reliable than buying capacity that looks impressive but does not match the work.
Frequently asked questions
What is the difference between a lathe and a turning center?
A lathe is the broader term for a machine that rotates a workpiece while a tool cuts it. A turning center usually refers to a CNC lathe designed for higher productivity, repeatability, guarding, automatic tool changing, and often additional capabilities such as live tooling, sub-spindles, or automated material handling.
Are manual lathes still useful in modern manufacturing?
Yes. Manual lathes remain useful for repair work, training, toolroom jobs, simple prototypes, and very low-volume parts. They are less suitable when a shop needs consistent repeatability, complex programs, documented process control, or high-volume production with limited operator intervention.
When should a shop consider a Swiss-type lathe?
A Swiss-type lathe is worth considering when parts are small, long relative to their diameter, and sensitive to deflection. It is common in industries that need precise small components. It is not the default choice for all turning work because setup, tooling, and part-family fit are highly specific.
What safety issue is most often underestimated on lathes?
Rotating workholding and protruding stock are often underestimated. Chucks, jaws, bar stock, and irregular fixtures can create entanglement or impact hazards. Guarding, safe setup procedures, operator training, and proper workholding review should be part of every turning process.
Is a mill-turn machine always better than a standard CNC lathe?
No. A mill-turn machine can reduce handling and improve accuracy between features when parts need both turning and milling. If parts are simple turned components, the added cost, programming complexity, and maintenance requirements may not be justified.