Plastic manufacturing processes explained for product design and production planning
Plastic manufacturing processes convert polymer materials into finished parts by melting, shaping, curing, forming or building plastic into a specified geometry. In practice, the right choice is rarely based on one headline cost. It depends on the part’s shape, annual volume, resin, tolerance requirements, surface finish, tooling budget and compliance risks. Injection molding is often suited to high-volume complex parts, extrusion to continuous profiles, blow molding to hollow containers, thermoforming to thin shells and trays, rotational molding to large hollow parts, compression molding to thermosets and composites, and additive manufacturing to prototypes or low-volume production. For more process comparisons, see our manufacturing processes category.
How plastic manufacturing processes turn resin into parts
Most plastic manufacturing starts with a polymer in pellet, powder, sheet, film, liquid resin or compound form. The material is heated, pressurized, formed, cured or cooled until it becomes a stable part. Equipment and tooling vary by process, but the production challenge is similar: control material flow, temperature, pressure, cooling rate, shrinkage and post-processing so the part meets its functional requirements.
Thermoplastics such as polyethylene, polypropylene, polystyrene, ABS, polycarbonate and nylon can generally be softened by heat and solidified again by cooling. That behavior makes them suitable for processes such as injection molding, extrusion, blow molding and thermoforming. Thermosets, including many phenolic, epoxy and unsaturated polyester systems, form cross-linked structures during curing and typically cannot be remelted in the same way. This difference affects equipment choice, cycle behavior, scrap handling and repair options.
For regulatory classification, the U.S. EPA describes the plastics and rubber products manufacturing sector under NAICS 326 as establishments that make goods by processing plastic materials and raw rubber. The agency also connects the sector with air-emissions references such as AP-42. This matters because process selection is not only a design decision; it can also affect permitting, ventilation, emissions estimation and waste management. (epa.gov)
Main plastic manufacturing processes compared
The table below summarizes the most common plastic manufacturing processes from a production-planning perspective. It does not replace a supplier quotation, mold-flow review or material trial, but it can help narrow the options before detailed engineering begins.
| Process | How it works | Typical products | Strengths | Key limits |
|---|---|---|---|---|
| Injection molding | Molten plastic is injected into a closed mold, cooled and ejected. | Housings, clips, caps, gears, medical and consumer components | High repeatability, complex shapes, strong output rate after tooling | High mold cost, design changes can be expensive, shrinkage must be controlled |
| Extrusion | Plastic is melted and pushed through a die to create a continuous shape. | Pipes, tubing, sheet, film, seals, profiles | Efficient for long constant cross-sections and continuous production | Limited to continuous profiles or downstream-formed products |
| Blow molding | A heated parison or preform is inflated inside a mold. | Bottles, tanks, containers, ducts | Good for hollow parts with relatively thin walls | Wall-thickness control and neck/handle geometry require careful design |
| Thermoforming | A heated plastic sheet is formed over or into a mold, then trimmed. | Trays, covers, packaging, panels, liners | Lower tooling cost than many molded alternatives; good for large thin parts | Trimming scrap, less detail than injection molding, wall thinning in deep draws |
| Rotational molding | Powdered resin rotates in a heated mold and coats the mold interior. | Large tanks, bins, playground parts, hollow housings | Large hollow parts with low internal stress and relatively simple tooling | Longer cycles and less precision than high-pressure molding |
| Compression molding | A measured charge is placed in a heated mold and compressed until formed or cured. | Thermoset parts, electrical components, composite panels | Suitable for thermosets and some reinforced materials | Flash, cure time and material handling must be managed |
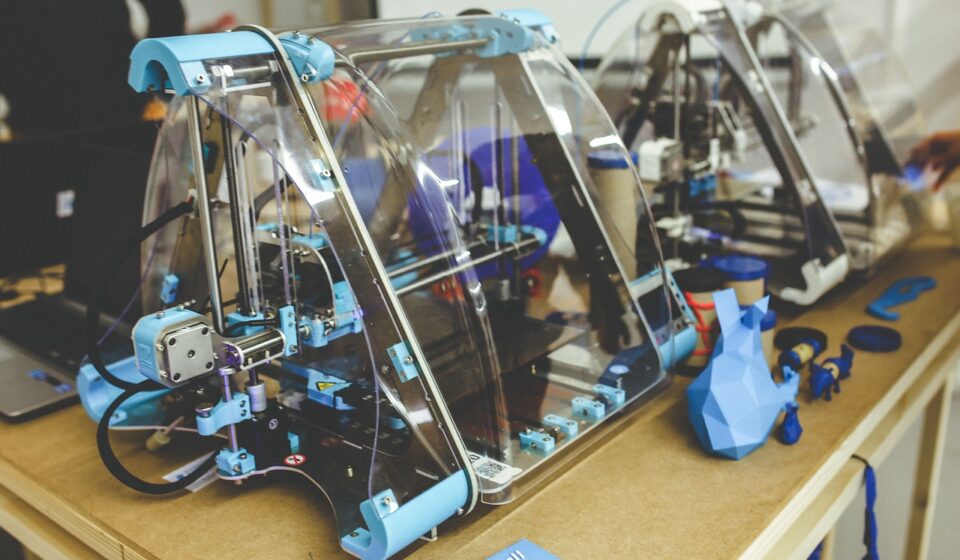
| Additive manufacturing | Parts are built layer by layer from filament, powder or resin. | Prototypes, fixtures, jigs, low-volume custom parts | Fast iteration and no hard tooling for many geometries | Material properties, surface finish and unit cost may limit mass production |
How to choose the right process for a plastic part
Start with production volume and tooling economics
Tooling cost is usually one of the first filters. Injection molding can deliver low unit cost at scale, but the mold, validation and revision costs can be significant. Thermoforming, rotational molding and some compression molding applications may use simpler tooling, which can make them attractive for lower volumes or larger parts. Additive manufacturing avoids hard tooling in many cases, but per-part build time and post-processing can become limiting as volume increases.
The practical question is not simply which process is cheapest. It is which process, at the expected production volume, can deliver the required quality with the lowest combined cost of tooling, cycle time, labor, scrap, inspection, packaging and change management.
Match geometry to the forming method
Part geometry often removes unsuitable options early. A bottle or fuel container points toward blow molding or rotational molding. A long seal, pipe or window profile points toward extrusion. A thin tray or enclosure cover may fit thermoforming. A small complex component with bosses, ribs, clips and controlled mating surfaces is often a candidate for injection molding.
Undercuts, threads, snap fits, living hinges, inserts, ribs, weld lines and assembly interfaces all matter. Some features can be molded directly. Others require slides, secondary machining, ultrasonic welding, heat staking or assembly operations. When the design works against the process, the result is more likely to be flash, sink marks, warpage, slow cycles or premature tool wear.
Consider material behavior before freezing the design
Plastics are not simply metals with lower stiffness. They respond differently to heat, moisture, load duration, cooling rate and orientation. Semi-crystalline materials generally shrink differently from amorphous materials. Filled materials may improve stiffness or heat resistance, but glass fiber or mineral fillers can also affect flow, weld-line strength, tooling abrasion and anisotropic shrinkage.
For molded plastic parts, ISO 20457:2026 addresses geometrical and dimensional tolerances and acceptance conditions for plastic molded parts, including processes such as injection molding, injection-compression molding, transfer molding, compression molding and rotational molding. Its scope is a useful reminder that plastic tolerancing should reflect material and process behavior rather than simply copying metal-part tolerance habits. (committee.iso.org)
Quality and design-for-manufacturing factors
Good plastic part design connects function with manufacturability. For injection molded parts, common DFM concerns include uniform wall thickness, rib proportions, draft angles, gate location, venting, knit lines, cooling balance and ejection forces. For thermoformed parts, designers pay close attention to draw depth, corner radii, sheet thickness and trimming strategy. For extruded products, die swell, cooling, puller speed and dimensional stability are central. For blow molded parts, parison programming and pinch-off design can determine whether wall thickness is acceptable in critical areas.
Quality planning should define what must be measured, how often it must be measured and which features truly affect performance. Critical-to-function dimensions, sealing surfaces, snap-fit engagement, optical surfaces, threaded areas, living hinges and safety-related features deserve more attention than nonfunctional surfaces. Over-tight tolerances can increase cost without improving performance, while vague drawings can push quality risk downstream. See also: buying guides.
- Wall thickness: sudden changes can create sink, voids, warpage or slow cooling.
- Draft: insufficient draft can damage surfaces or raise ejection force.
- Radii: sharp internal corners can concentrate stress and reduce flow quality.
- Gates and weld lines: their location can affect appearance and strength.
- Cooling: uneven cooling often drives warpage and cycle-time variation.
- Material conditioning: some resins require drying or controlled handling before processing.
Environmental, safety and compliance considerations
Plastic manufacturing processes can involve hot surfaces, moving platens, rotating screws, high clamp forces, trimming blades, fumes, dust, resins, additives and cleaning chemicals. OSHA’s plastics machinery guidance discusses machinery categories such as horizontal injection molding machines, blow molding machines and roll-forming equipment, and its plastics-industry standards page highlights machine guarding and related safety requirements. (osha.gov)
Environmental controls depend on the resin, additives, process temperature, cleaning method and facility layout. Extrusion and injection molding of thermoplastics may have different emission profiles from open-mold composite fabrication or solvent-intensive secondary operations. Scrap handling also varies. Clean thermoplastic runners, sprues and trim may sometimes be reground under controlled conditions, while contaminated, degraded, reinforced or thermoset waste may require different handling.
From a planning standpoint, sustainability claims should be treated cautiously. A process may reduce tooling waste but increase energy use. A recyclable resin may be difficult to recycle after pigments, adhesives, fillers or mixed-material assembly. A lighter plastic part may reduce shipping weight but create end-of-life challenges. Useful process comparisons should state the boundary of the claim instead of relying on broad labels such as green or eco-friendly without evidence.
Practical checklist for process selection
Before requesting quotations or finalizing a drawing, teams can use a short checklist to avoid mismatches between design and production method.
- Define the part function: load, temperature, chemical exposure, appearance, sealing and service life.
- Estimate production volume: prototype, bridge production, annual production and expected product life.
- Select candidate materials: include mechanical, thermal, electrical, regulatory and cost requirements.
- Screen viable processes: compare geometry, wall thickness, tolerance and surface needs.
- Review tooling impact: consider mold cost, lead time, revision risk and maintenance.
- Plan secondary operations: trimming, machining, welding, decorating, assembly and inspection.
- Check compliance needs: machine guarding, ventilation, emissions estimation, waste handling and material documentation.
- Validate before scaling: use prototypes, design reviews, first-article inspection and process capability evidence where appropriate.
The best choice is usually the process that creates the required part with the fewest compromises across geometry, material performance, repeatability, cost and compliance. In many projects, the strongest result comes from adjusting the part design slightly so it works with the process, rather than forcing the process to rescue a difficult design.
Frequently asked questions
What are the most common plastic manufacturing processes?
The most common processes include injection molding, extrusion, blow molding, thermoforming, rotational molding, compression molding and additive manufacturing. The right choice depends on whether the part is solid, hollow, continuous, sheet-like, large, thin-walled, highly detailed or produced in low or high volume.
Which plastic manufacturing process is best for high-volume parts?
Injection molding is often preferred for high-volume plastic parts when the design needs complex geometry, repeatable dimensions and fast cycles after tooling is built. However, extrusion may be better for continuous profiles, and blow molding may be better for high-volume hollow containers.
Which process has the lowest tooling cost?
Additive manufacturing usually avoids hard tooling, while thermoforming and rotational molding often use lower-cost tooling than complex injection molds. The lowest total cost still depends on part size, quantity, material, labor, cycle time, scrap and post-processing.
Why do plastic parts need different tolerances from metal parts?
Plastic parts shrink, expand, absorb moisture and deform differently from metal parts. Material grade, wall thickness, mold temperature, cooling rate, fiber orientation and processing conditions can all affect dimensions. This is why plastic-specific tolerance planning is important for molded components.
Can one plastic part use more than one manufacturing process?
Yes. A product may combine injection molded housings, extruded seals, thermoformed covers, machined prototypes, 3D printed fixtures or welded subassemblies. Process selection should consider the complete product architecture, not only a single component.