Axis precision engineering components and the real drivers of motion accuracy
Why axis precision is a system property
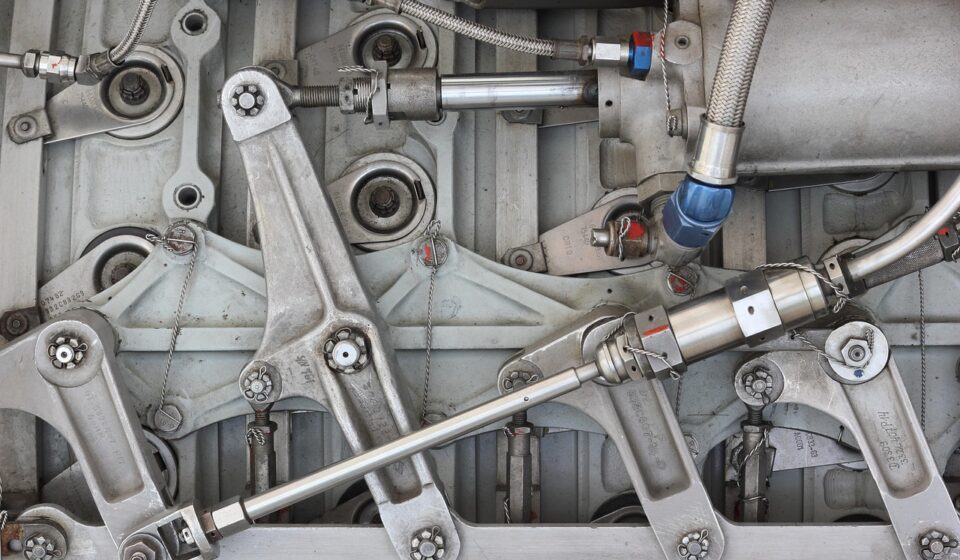
Axis precision engineering components are the mechanical and feedback elements that determine how reliably a controlled axis can move, stop, and return to position. In machine tools, robots, inspection systems, and automated handling equipment, axis precision does not come from one “high accuracy” part. It comes from a chain of parts and conditions: guideways, bearings, screws or racks, couplings, motor and encoder mounting, structural stiffness, lubrication, thermal behavior, control tuning, and verification. For engineers, the practical question is not whether a component is precise in isolation. It is whether the assembled axis can meet the required positioning, geometry, load, speed, and inspection method under real operating conditions.
That distinction matters because an axis is a functional assembly. A ground ball screw with low lead error can still perform poorly if its end bearings are misaligned, the linear guide preload is inconsistent, or thermal growth is ignored. A rigid bearing block cannot compensate for a weak mounting surface or unclear drawing datums. Good precision engineering therefore starts with the motion requirement and works backward through the component chain.
What counts as an axis precision component
In manufacturing, an “axis” usually means a controlled linear or rotary direction of motion. A three-axis machining center has X, Y, and Z linear axes. A five-axis system adds rotary axes. A robot may have several rotational joints whose combined movement determines tool or gripper position. In each case, the axis is more than the actuator. It includes the surfaces and parts that guide, support, transmit, measure, and restrain motion.
The most common axis precision engineering components include:
- Linear guides and slideways that constrain straight-line travel and resist yaw, pitch, roll, and side loading.
- Ball screws, lead screws, racks, pinions, belts, and direct-drive elements that convert motor output into controlled motion.
- Angular contact bearings, crossed roller bearings, rotary tables, and spindle bearings that support radial, axial, and moment loads.
- Couplings, motor mounts, bearing housings, and support blocks that connect the drive train while controlling misalignment and stiffness loss.
- Encoders, scales, resolvers, and reference sensors that provide position feedback to the controller.
- Structural interfaces such as precision-machined bases, rails, pads, datum surfaces, and fastener patterns.
Each part has its own tolerance. The final axis performance, however, depends on how those tolerances stack up, how loads move through the structure, and how the system is measured after assembly.
The component chain behind one accurate axis
Guidance and constraint
Guidance components define the path of motion. Linear guides, box ways, hydrostatic ways, air bearings, and crossed roller systems all reduce unwanted degrees of freedom, but they do it with different trade-offs. Rolling guides can offer compact size and load capacity. Fluid or air bearing systems may reduce friction and stick-slip in specialized equipment. The key issue is not simply low friction; it is whether the guide arrangement maintains straightness, parallelism, and stiffness over the required travel and load range.
Mounting surfaces are often the overlooked part of guidance accuracy. A precision rail installed on a distorted base can inherit that distortion. Bolt tightening sequence, rail datum edges, support-surface flatness, and cleanliness during assembly can all affect the result. For this reason, axis precision should be specified at both the component level and the assembled-axis level.
Drive transmission and lost motion
The drive system determines how commanded motion becomes actual movement. Ball screws are widely used because they combine efficiency with controlled lead accuracy, but backlash, end support stiffness, nut preload, screw whip, and thermal expansion can still affect positioning. Rack-and-pinion systems may be better suited to long travel. Direct-drive linear motors remove some mechanical transmission errors, but they place more importance on feedback resolution, thermal control, and structural design.
Lost motion is especially important when an axis reverses direction. Backlash in screws, compliance in couplings, looseness in bearing seats, or micro-movement at interfaces can make an axis repeat differently depending on the approach direction. In practical inspection, bidirectional positioning tests can reveal issues that a one-direction check may miss.
Feedback, control, and the mechanical loop
Position feedback closes the control loop, but the sensor location matters. A motor encoder measures motor rotation. A linear scale measures table or slide position more directly. If the feedback device is far from the point of work, mechanical compliance between the sensor and the tool center point may remain invisible to the controller. This is why high-end motion systems often treat feedback selection as part of the mechanical design, not just an electronics choice.
Control tuning also has limits. Servo gains can improve response, but they cannot fully remove structural resonance, weak joints, poor bearing support, or thermal drift. In precision engineering, control performs best when the mechanical loop is already stiff, repeatable, and properly constrained.
How standards frame accuracy, repeatability, and tolerancing
Precision discussions become vague unless the required characteristic is clearly defined. Accuracy, repeatability, straightness, flatness, circularity, run-out, backlash, and resolution are related, but they are not interchangeable. Public standards help engineers separate these terms and turn them into testable specifications.
| Engineering question | Why it matters for axis components | Relevant reference framework |
|---|---|---|
| Can the axis reach commanded positions repeatedly? | Positioning performance must be checked across travel, approach direction, environment, and warm-up condition, not only at one point. | ISO 230-2 covers the determination of accuracy and repeatability of positioning for numerically controlled axes. (iso.org) |
| Is the machine geometry controlled? | Axis components can meet catalog tolerances while the assembled machine still has straightness, squareness, or geometric errors. | ISO 230-1 specifies methods for testing geometric accuracy of machine tools under no-load or quasi-static conditions. (iso.org) |
| Are drawings and datums unambiguous? | Precision parts need clear tolerancing language for form, orientation, location, and run-out. | ISO 1101:2017 defines the symbol language and interpretation rules for geometrical tolerancing of workpieces. (iso.org) |
| Are shaft and hole fits consistently defined? | Bearing seats, guide supports, motor pilots, and coupling bores often depend on standardized fit language. | ISO 286-1 establishes the ISO code system for tolerances on linear sizes for cylinders and two parallel opposite surfaces, while ISO 286-2 provides tables of limit deviations for common hole and shaft classes. (iso.org) |
| Can inspection equipment verify the requirement? | A tolerance is useful only when the measurement method and instrument capability are suitable for the feature being checked. | ISO 10360-2 specifies acceptance and reverification tests for Cartesian CMMs used to measure linear dimensions. (iso.org) |
For robots and multi-axis handling systems, the distinction between pose accuracy and repeatability is also important. ISO 9283 describes test methods for performance characteristics such as pose accuracy, pose repeatability, path accuracy, stabilization time, overshoot, and static compliance for manipulating industrial robots. (iso.org)
Design choices that often matter more than a tighter catalog tolerance
A common mistake is to specify the tightest available component grade without checking whether the rest of the system can benefit from it. In many axis assemblies, the limiting factor is not the nominal precision grade of one purchased part. It may be the flatness of the mounting base, bearing spacing, thermal expansion, lubrication control, cable forces, or the way the load is applied.
Preload and stiffness are good examples. Preload can reduce clearance in bearings, guides, and ball screws, but excessive preload can increase friction, heat, wear, and drive load. The right preload is application-specific: a lightly loaded inspection axis, a high-force machining axis, and a fast pick-and-place axis do not have the same stiffness, heat, and life requirements.
Thermal behavior is another major driver. Motors, screws, bearings, and ambient changes can all introduce expansion. A component that measures correctly at inspection temperature may shift during operation if heat sources and expansion paths are not controlled. Precision assemblies therefore need attention to warm-up strategy, material choices, heat dissipation, and the location of feedback devices. See also: buying guides.
Datum strategy can be more valuable than an isolated micron-level feature. If drawings do not identify the functional datums that locate the rail, bearing, screw, sensor, and tool path, inspection may confirm individual dimensions while missing the relationship that controls motion. GD&T helps connect the component drawing to assembly function when it is applied with a clear datum scheme rather than used as decoration.
Surface integrity also matters. Bearing seats, rail lands, and precision sliding surfaces need more than dimensional size control. Roundness, waviness, surface texture, residual stress, burr control, and edge condition can affect how parts seat and how loads are distributed. ISO 21920-1 is part of the GPS framework for indicating surface texture on technical product documentation. (iso.org)
Inspection planning for precision axis parts
Inspection should be planned before manufacturing, not added after parts are cut. The first step is to identify which features actually control the axis function. A bearing bore may need size, roundness, cylindricity, and location relative to a datum face. A rail mounting surface may need flatness, parallelism to a second rail surface, hole pattern location, and burr-free edges. A screw support block may need bore alignment to the mounting face and to the opposite support.
The second step is to choose a measurement method that matches the tolerance. CMMs, height gauges, surface plates, bore gauges, air gauges, roundness testers, laser interferometers, autocollimators, and surface texture instruments all serve different purposes. No single instrument is ideal for every precision component. For assembled motion axes, laser-based positioning tests, ballbar tests, straightedge checks, or machine-specific geometric tests may reveal behavior that component inspection alone cannot show.
Measurement traceability also needs careful wording. NIST explains metrological traceability in terms of a measurement result connected to a reference through a documented chain of calibrations, with each link contributing to measurement uncertainty. It also emphasizes that uncertainty must be calculated using a well-established method rather than assumed from an instrument label alone. (nist.gov)
This has a practical consequence for axis precision engineering components: a supplier certificate, a calibrated CMM, or a tight drawing tolerance does not by itself prove that a functional motion requirement has been met. The measurement method, environmental conditions, uncertainty budget, and acceptance rule should be suitable for the tolerance being claimed.
Implications for sourcing and specification
When comparing axis precision components, engineers should move from catalog claims to functional questions. The following checklist is a useful starting point for component selection, drawing review, and supplier discussion:
- What is the required axis-level performance: positioning accuracy, repeatability, straightness, stiffness, speed, load capacity, or thermal stability?
- Which component features directly control that performance?
- Are datums, fits, geometric tolerances, and surface texture requirements stated in a way that can be inspected?
- Will the assembly process preserve the precision of the individual parts?
- Is the feedback device measuring the controlled point or only the actuator?
- What warm-up, lubrication, preload, and environmental assumptions are included?
- Which acceptance test proves the requirement at the component and assembled-axis levels?
For readers comparing related motion and machined-part topics, the precision components category collects additional manufacturing and engineering background. The central lesson is consistent across applications: specify the axis function first, then select components, tolerances, and inspection methods that support that function.
Frequently asked questions
Are axis precision engineering components the same as CNC machine parts?
They overlap, but they are not identical. CNC machines use many axis precision components, including guideways, screws, bearings, rotary tables, and feedback devices. The same engineering principles also apply to inspection equipment, semiconductor handling, automation stages, robotics, packaging machinery, and other controlled-motion systems.
Is repeatability more important than accuracy?
It depends on the application. A process that can be calibrated or offset may rely heavily on repeatability. A system that must move to an absolute location without frequent compensation needs stronger accuracy. Robotics standards such as ISO 9283 treat accuracy and repeatability as distinct performance characteristics, which is a useful reminder not to combine them into one vague “precision” number. (iso.org)
Can a high-precision ball screw guarantee an accurate axis?
No. A precision screw can reduce one source of positioning error, but axis accuracy also depends on support bearings, mounting alignment, guide geometry, preload, thermal growth, feedback location, and control behavior. The assembled axis should be verified with a suitable positioning or geometric test.
Why do precision drawings use GD&T instead of only plus-minus tolerances?
Plus-minus tolerances can define size or simple dimensional limits, but many axis components depend on relationships between features: perpendicularity of a bearing face, position of mounting holes, parallelism of rail lands, or run-out of a rotating seat. GD&T provides a structured way to define those relationships when the datum scheme is chosen correctly.
What is the biggest specification mistake in precision axis components?
The biggest mistake is specifying tight component tolerances without defining the axis-level acceptance requirement. A better specification connects the functional motion requirement to component tolerances, assembly controls, measurement uncertainty, and a verification method that reflects real operating conditions.